
Maintenance Overview
Most downtime on a mobile crushing plant is not the machine breaking down. It is the crew waiting for a part. A worn jaw plate, a cut conveyor belt, a blocked filter element - if the spare is not on the shelf, the whole line sits idle.
- Buy wear parts ahead of the wear rate, not after failure - Split spares into three tiers: must-stock, recommended, on-demand - Retire parts by measurement, not by looks - Cleaning, torque and run-in during change-out decide how long the next set lasts
In the stoppage records Vanguard Machinery has collected from sites over the past few years, more hours were lost waiting for spares than were spent on actual overhauls. This guide goes through what really wears on a mobile plant, system by system, along with stock levels, retirement criteria and the practical steps that keep a parts change from turning into a comeback job.
Where the Wear Happens: Five Systems on One Chassis
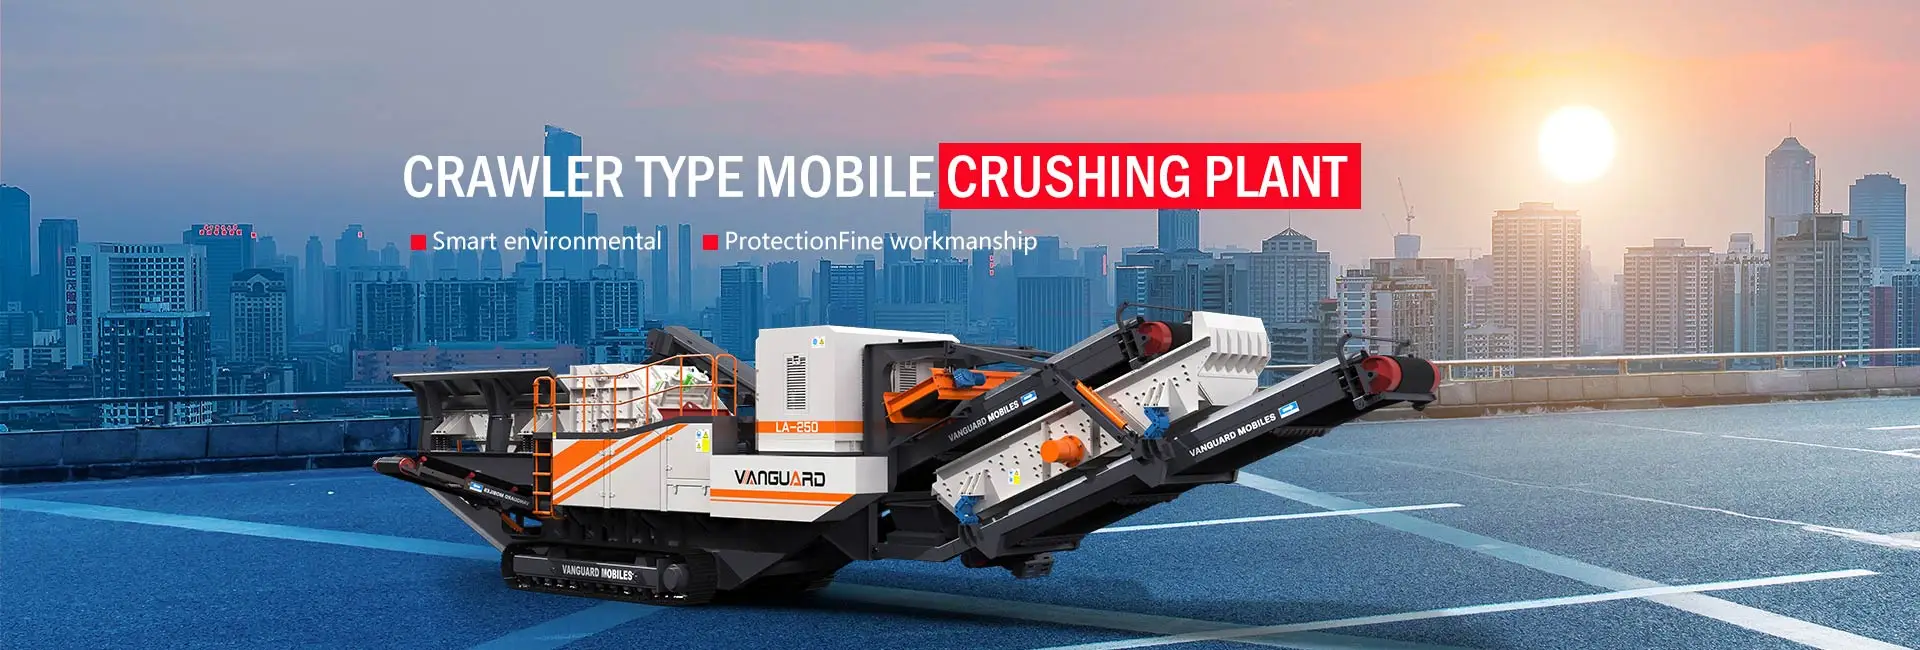
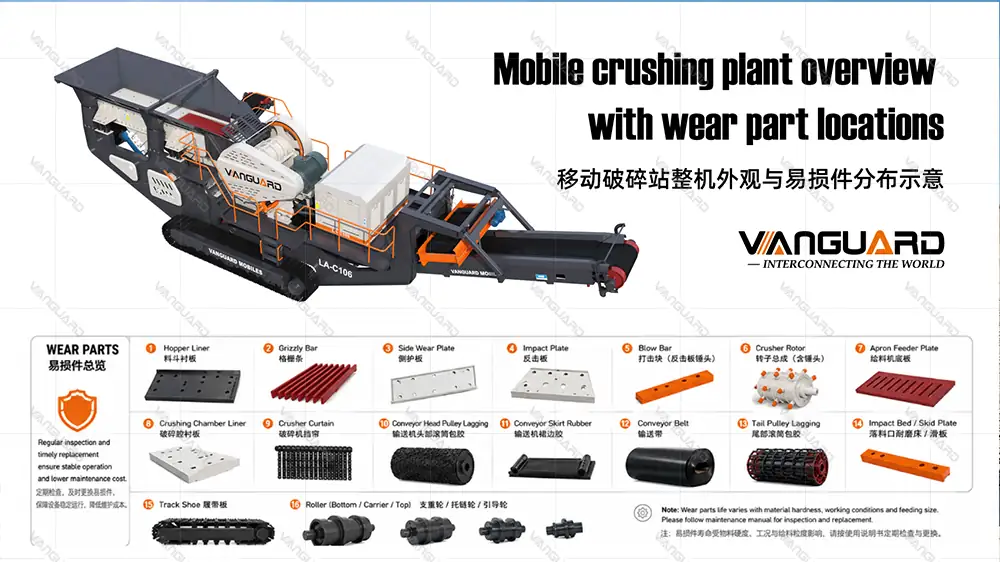
A mobile crushing plant puts feeding, crushing and discharge conveying on one chassis. It looks like a single machine, but five systems are wearing at the same time:
- Crushing chamber - takes the rock directly, wears fastest, costs the most - Screening unit - mesh, liners, bounce balls - Discharge conveying - belt, idlers, belt cleaner blades - Drive and power - drive belts, couplings, bearings - Hydraulics and electrics - oil, filters, seals, hoses
Sort your spares across these five and nothing gets missed. Plenty of sites watch the chamber only, then lose a full day to a torn conveyor belt.
Chamber Wear Parts: Jaw Plates, Blow Bars, Liners
The chamber is where the money goes, and where stocking mistakes hurt most. The parts depend entirely on the crusher type:
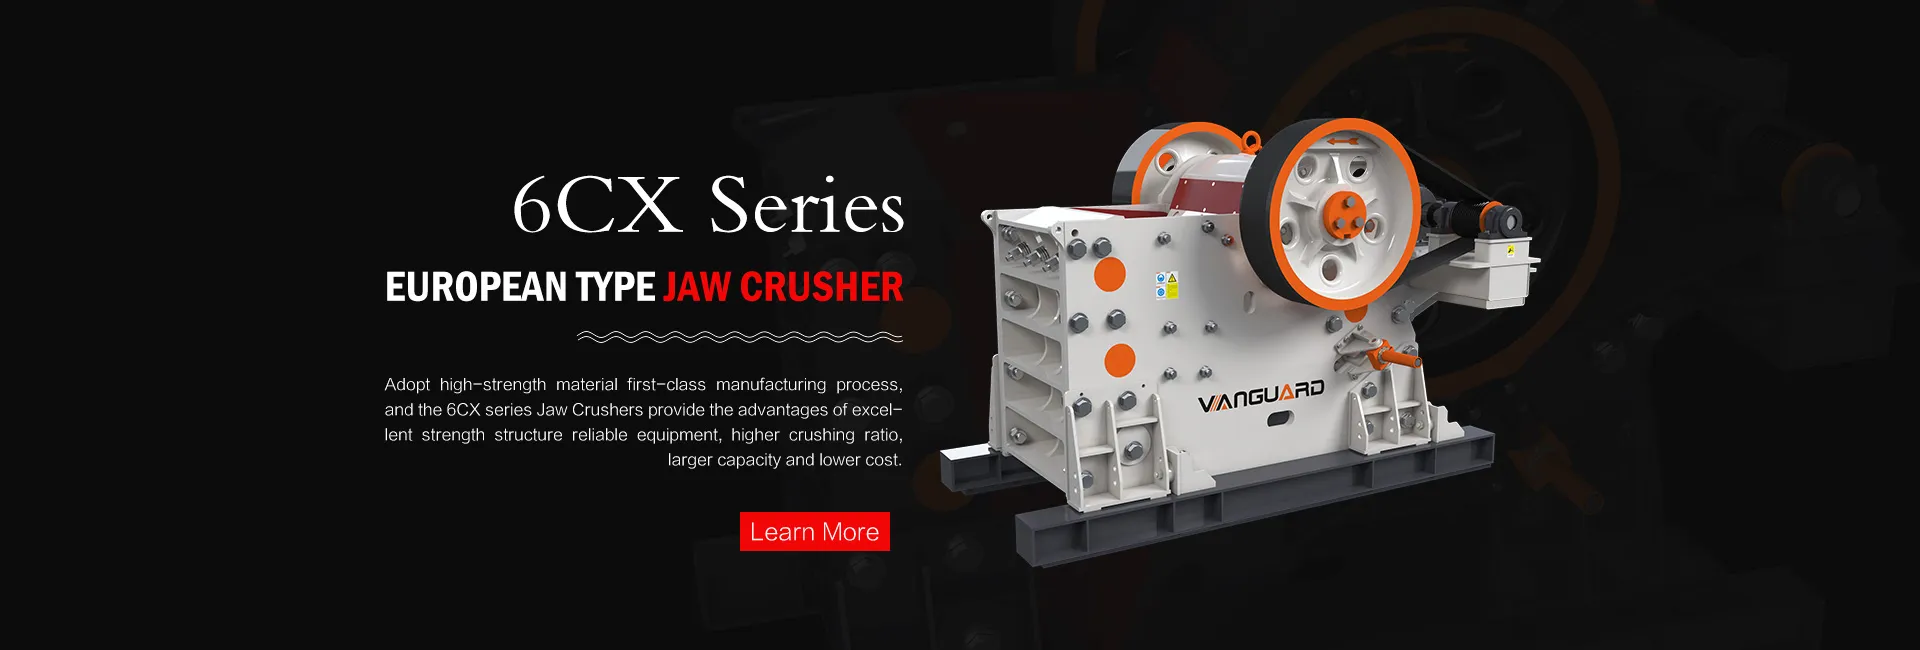
- Jaw: swing jaw plate, fixed jaw plate, toggle plate, toggle seat, tension rod spring - Impact: blow bars, impact aprons, grinding path plates - Cone: mantle, concave, main shaft bushing, dust seal - VSI: rotor, feed tube, distributor plate, wear tips
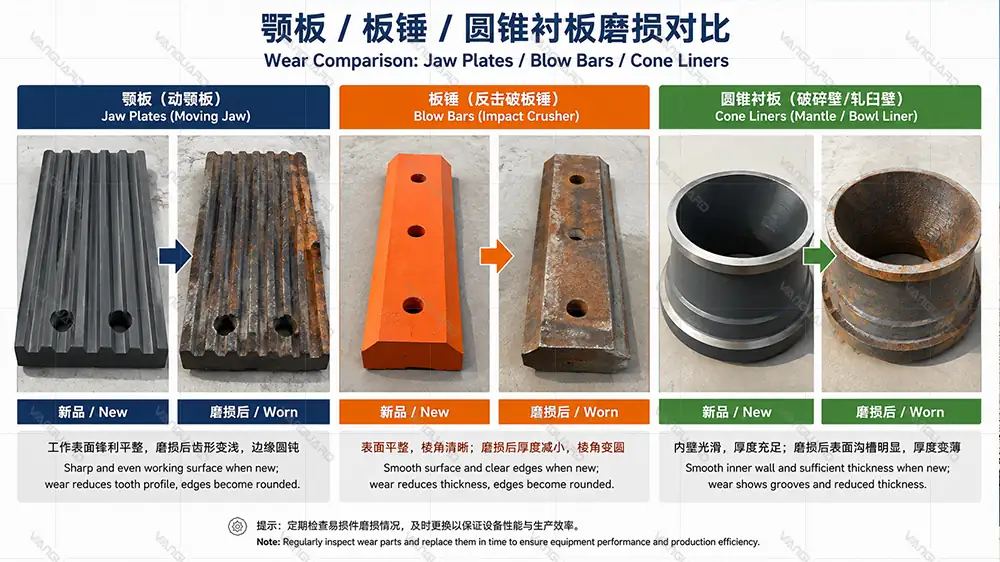
On a Crawler Type Mobile Jaw Crushing Plant, jaw plates and toggle plates are must-stock. Move to a Crawler Type Mobile Impact Crushing Plant and blow bars plus aprons take over, and blow bars go far faster than jaw plates. On a Crawler Type Mobile Cone Crushing Plant, mantle and concave get replaced as a pair, because changing only one gives you an uneven chamber and wrecks both faster.
The trap here is stocking by machine model. Run hard rock one month and soft rock the next and the wear rate swings two or three times. The old stocking rule breaks the moment the first hard-rock month lands and the shelf is empty.
Retirement is not about thin metal. A jaw plate gets changed when the tooth profile flattens, the closed side setting will not close any further, or throughput drops below about 80 percent. A blow bar gets flipped or replaced once it has lost roughly a third of its weight, or once the corners round off and product shape suffers. A cone liner is measured at its thinnest point, and you check for uneven wear at the same time, because uneven wear usually means off-centre feed or inconsistent feed size.
Vanguard Machinery field engineers usually ask for three months of measurements before drawing any conclusion. Log the numbers at every stoppage for the first quarter, plot your own wear curve, and after that you stock against your own duty instead of a catalogue figure.
Screening and Conveying Wear Parts
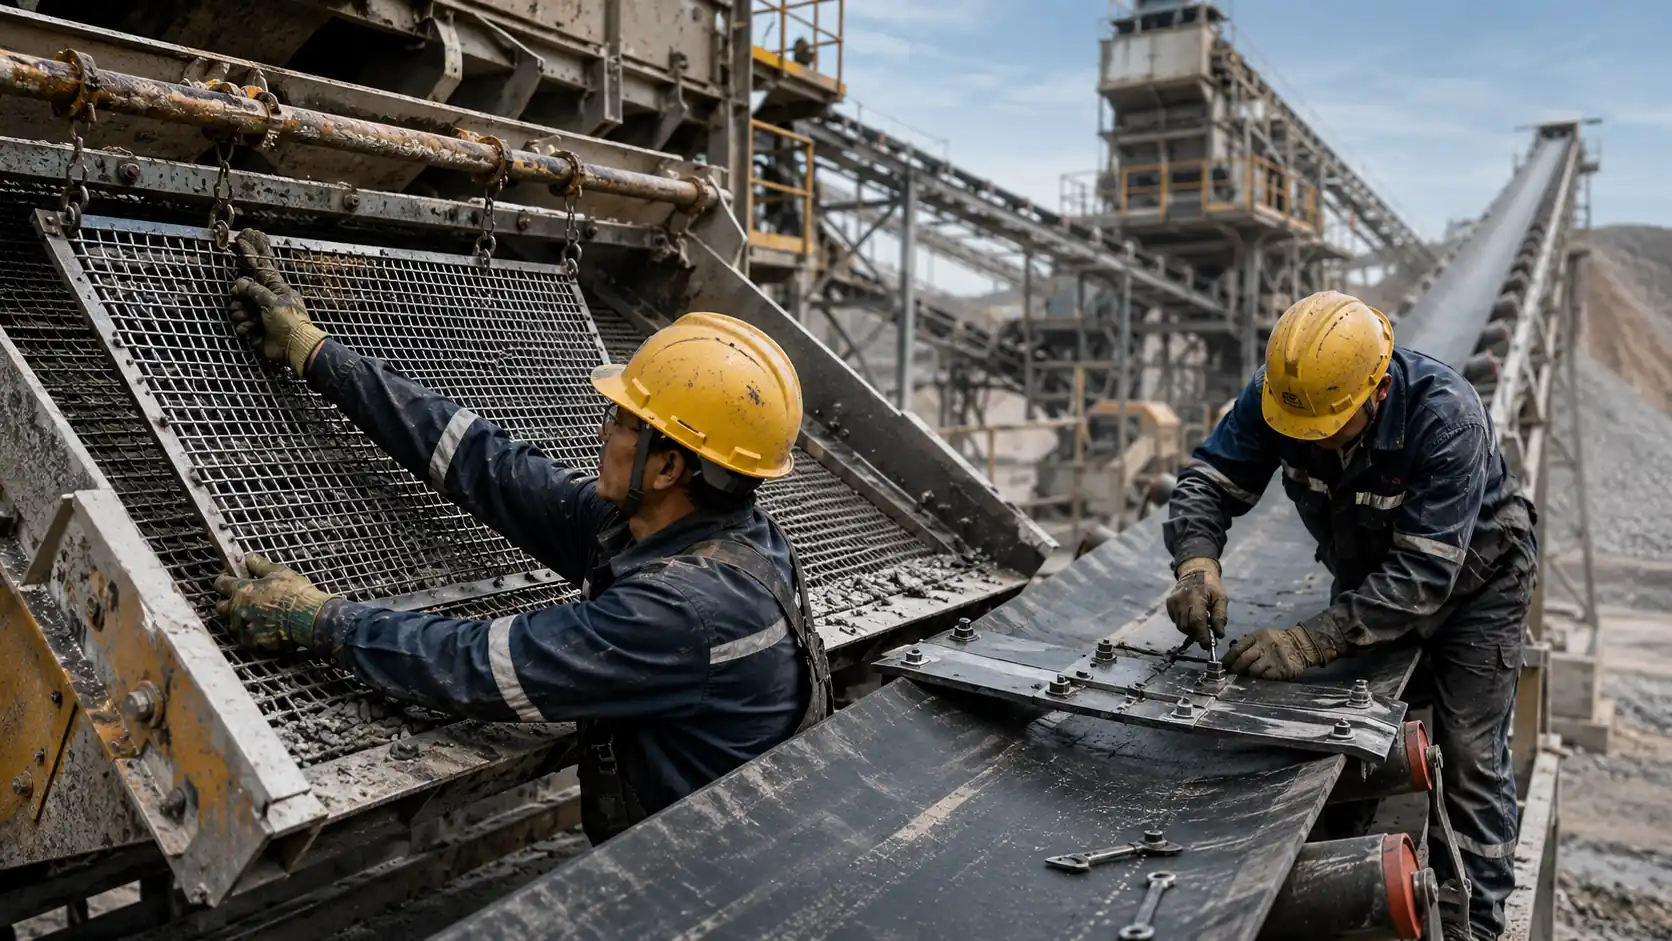
Screening wear parts tend to get ignored right up until product gradation goes off spec.
- Screen mesh - check hole wear and blinding. Worn holes let oversize straight into the product - Mesh clamping and bounce balls - once the balls lose their bounce, blinding climbs fast - Screen and chute liners - the impact point wears first, and wear plate stretches it out - Conveyor belt - look for cuts, delamination and splice lift. The splice is the weak spot - Idlers and pulleys - change the seized and noisy ones first. One seized idler cuts through a belt quickly - Belt cleaner blades - carry-back accelerates wear on idlers and pulleys alike
A full belt is too big to stock and rarely worth it. Stock the things that save the belt instead: splice material, cold-cure rubber, repair patches and a handful of common idlers. A half-hour field repair beats a two-day wait for a replacement belt.
The Vanguard Machinery spare parts list for a mobile unit keeps screening and conveying on a separate page for exactly this reason: they are the two most often forgotten.
Drive, Power and Hydraulic Wear Parts
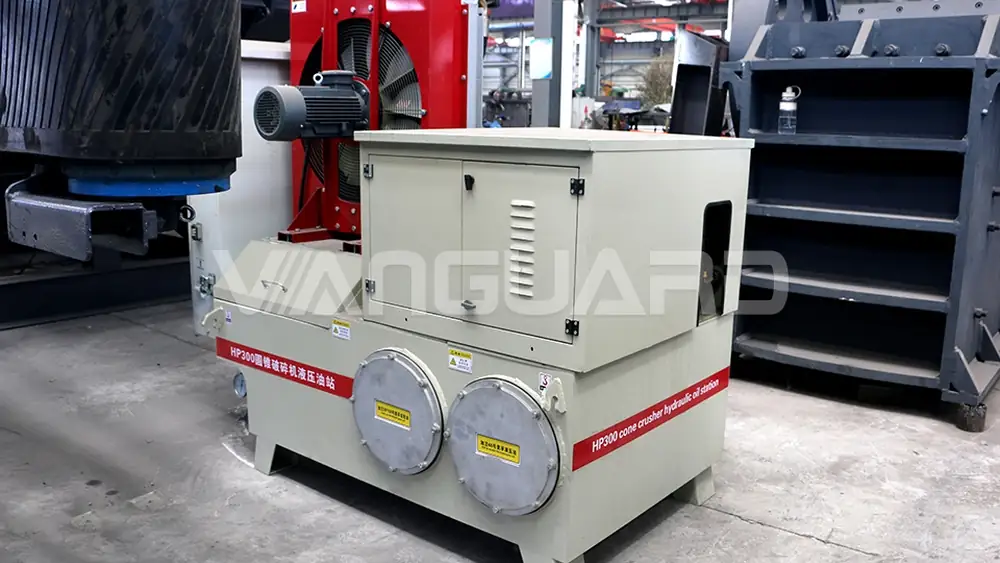
- Drive belts - cracks, slip, tension. Re-tension once after the run-in - Coupling inserts - cheap, but the machine stops when they let go, and noise is the warning - Bearings - judge by temperature and vibration, not by noise. More than 40 degrees above ambient, or a clear jump in vibration velocity, means investigate - Hydraulic oil and filters - go by hours or differential pressure, whichever comes first. A blocked filter opens the bypass and dirty oil goes straight through the system - Seals and hoses - chase any seepage early. A bulging hose gets changed before it bursts - Electrics - loose terminals and burnt contactor faces show up fast on dusty sites
A VPE mobile crushing plant adds tyres, brakes and outrigger cylinder seals to the list, because it travels on wheels and levels on outriggers. Crawler units add track shoes, rollers and sprocket segments. It is a different walking gear, but the outcome when it fails is identical: you stop. Keep a separate list per machine type rather than mixing them together.
Three-Tier Spares List
| Tier | Part | Suggested stock | Reasoning |
| Must-stock | Core chamber parts (jaw plates / blow bars / liners) | One set fitted, one set spare | Stops production, long lead time |
| Must-stock | Screen mesh (common sizes) | 2 of each | Gradation goes off spec the moment it wears |
| Must-stock | Hydraulic, air and oil filter elements | 2 sets each | Differential pressure alarm means change now |
| Must-stock | Belt repair material, common idlers | 1 repair kit, 5-10 idlers | Handled on site in minutes |
| Recommended | Drive belts, coupling inserts | 1 set | Cheap, small, and the plant stops without them |
| Recommended | Seals, hose fittings | Assorted common sizes | Seepage is constant, replacement is frequent |
| Recommended | Toggle plate, tension rod spring (jaw) | 1 set | Consumed after tramp iron events |
| On-demand | Bearings, main shaft bushing | Assess by running hours | High unit cost, depends on age and duty |
| On-demand | Full conveyor belt | Do not stock, secure a supply channel | Ties up cash, emergency item needs fast delivery |
The three-tier split is simple: put your money into the parts that stop production, keep a set of the cheap failure-prone items on hand, and for expensive emergency items do not tie up cash but lock in a supplier who can ship fast.
Replacement Intervals and Retirement Criteria
| Wear part | Reference life | Retirement or change signal |
| Jaw plates | Hard rock 300-600 h; medium 800-1200 h | Tooth profile flat, CSS will not close, throughput below 80% |
| Blow bars | Abrasive 150-300 h; limestone 400-800 h | About one third of weight gone, corners rounded, shape suffers |
| Cone liners | 600-1500 h | Thinnest point at limit, uneven chamber, abnormal power draw |
| VSI wear parts | 200-800 h | Tips worn through, rotor body worn, fineness modulus drifting |
| Screen mesh | 3-9 months | Holes worn oversize, blinding up, oversize in product |
| Conveyor belt | 12-24 months | Cut reaching the carcass, delamination, splice lift |
| Idlers | 12-18 months | Seized, noisy, shell worn through |
| Drive belts | 3-6 months | Cracks, slip, no adjustment left |
| Hydraulic oil | 2000 h or 6 months | Sample out of spec, acid number up, water present |
| Filter elements | 500 h or differential pressure alarm | Alarm triggered, bypass open |
Treat these as reference ranges. Your own data is what counts. Feed abrasiveness, feed size, load factor and maintenance quality can each stretch or halve a service life. Build your own wear curve over the first three months and it will beat any table.
Vanguard Machinery ships a duty-based spares recommendation with every machine, but treat that as a starting point rather than a final answer. After three months of running, rewrite it using your own numbers.
Change-Out: Safety, Assembly, Run-In
1. Stop the machine, isolate and tag out, depressurise the hydraulics, confirm everything is fully stopped before anyone reaches in 2. Clean out the chamber and the dust. Plenty of bolts go missing because they are buried in material 3. Photograph and mark before you strip it, especially paired parts. Note the order and orientation 4. Inspect the seats. The wear part is not the only thing that deforms, so check seats, wedges and clamps 5. Torque to spec in stages and in a cross pattern. Not by feel, and not all in one go 6. Run in empty first, recheck torque and temperature, then load up gradually 7. Log the date and the hour reading. That is the raw data for your wear curve
One worth calling out separately: keep someone on the machine for the first eight hours after a change. Nearly every early failure shows up in that window, whether it is a loose bolt, an unseated part or a missed grease point. Once you are past eight hours, a problem usually means the new part is already damaged.
What Vanguard Machinery field engineers most often end up doing on site is simply sitting with the machine through those first eight hours.
Lubrication and Sealing: Getting More Hours from Wear Parts
- More grease is not better. Over-greasing raises temperature and grabs dust, and that wears parts faster - Point, quantity, interval. Put it in a table and log who did what and when - On dusty sites, wipe the fitting before you pump. A file costs less than a bearing - Failed sealing is the number one bearing killer. Dust seals, oil seals, labyrinths, chase any seepage - Use the specified brand and viscosity grade. Mixing grades causes trouble - Drain old oil completely. What settles at the bottom of the tank does more harm than the oil itself
On high-speed rotor machines such as the 5X vertical shaft impact crusher, lubrication and sealing are even less forgiving. One wrong grease grade or one missed interval can cost you a complete rotor.
Fault Quick Reference
| Symptom | Likely cause | Action |
| Throughput falling steadily | Worn parts, closed side setting opened up | Measure the chamber, adjust the setting or change the parts |
| Product shape getting worse | Blow bar corners rounded, uneven chamber wear | Flip or replace blow bars, check feed is centred |
| Oversize in product | Mesh worn or torn | Replace mesh, check the clamping |
| Loud running, heavy vibration | Tramp iron, loose liner, failing bearing | Stop and check fasteners first, then bearings |
| Bearing running hot | Poor lubrication, failed seal, over-tight fit | Check oil level and condition, inspect seal and clearance |
| Hydraulics slow or low pressure | Blocked filter, low oil, internal leak | Change filter, top up, check relief valve and cylinder seals |
| Belt tracking off | Seized idler, bad splice, off-centre loading | Realign idlers, redo the splice, fix the loading point |
| Oil milky | Water ingress or cooler leaking internally | Check cooler and breather, change the oil |
| Repeated blockages | Wet material, screening capacity short, setting too tight | Open the setting, check screening, control feed moisture |
| Power draw climbing | Worn parts, uneven load, belts slipping | Measure current, check chamber profile and belt tension |
FAQ
By duty, not by calendar. The same jaw plates can hit their limit at 300 hours in granite and run past 1000 hours in limestone. Log the measurements at every stoppage for the first three months, plot your own wear curve, and stock against that instead of a published figure.
Work in three tiers. Must-stock covers whatever stops production and takes a long time to buy, such as core chamber parts, filters and mesh, at one fitted plus one spare. Recommended covers the cheap, compact items that stop the plant when they fail, like drive belts and seals, one set on hand. On-demand covers expensive emergency items such as bearings and a full belt, where you do not tie up cash but you do secure a supplier who ships fast.
The crushing and screening side is largely the same, and the difference sits in the running gear. Crawler units need track shoes, rollers and sprocket segments watched. Wheeled units need tyres, brakes and outrigger cylinder seals. Keep one list per machine type rather than a single mixed list.
Set measuring points and let the numbers decide. Jaw plates are judged on tooth profile and how much setting adjustment is left, blow bars on weight loss and corner condition, cone liners on thickness at the thinnest point plus uneven wear, and mesh on hole size and blinding rate. Throughput dropping below about 80 percent of rating is a reliable change signal across the board.
Three things. Safety, meaning isolate, tag out and depressurise. Cleanliness, meaning the mating faces and seats are cleaned properly. Torque, meaning tightened to spec in stages and in a cross pattern, never by feel. Then run in empty, keep someone watching for the first eight hours, recheck torque and temperature, and only then load up.
No. Over-greasing raises temperature and pulls in dust, which wears parts faster. Log point, quantity and interval in a table, and wipe the fitting before pumping on dusty sites. Failed sealing is the number one bearing killer, so deal with seepage straight away rather than waiting.
Conclusion
Wear part management on a mobile plant comes down to three things: knowing which parts will wear, working out from your own duty when they reach the limit, and having them on the shelf before you need them. The list does not have to be long, but the must-stock items have to be complete, meaning jaw plates or blow bars, screen mesh, filter elements and belt repair material. Miss any one of those four and you have bought yourself a day of downtime.
The Vanguard Machinery recommendation is straightforward: spend the first three months building your own wear curve, then stock against that curve and carry out every change with proper torque and clean mating faces. When hard rock duty or a capacity increase comes round, top the spares up one cycle early. That is always cheaper than chasing a shipment after the line has already stopped.
Related Articles
• From Zhengzhou to Almaty: Vanguard Machinery to Exhibit at the 31st Kazakhstan K(2026-08-06)
• Vanguard Machinery to Exhibit at Construction Indonesia 2026, Deepening Its Sout(2026-08-06)
• The First Stage That Sets the Tone: Vanguard Machinery Brings the Tracked Mobile(2026-08-06)
• How to Choose a Mobile Crushing Plant Manufacturer...(2026-08-27)
• Best PFV1315 Impact Crusher for Limestone Crushing in Saudi ...(2026-08-06)
• How to Maintain a Crawler Type Mobile Jaw Crushing Plant(2026-08-05)
• Top 5 Reliable Crusher Alternatives to European Br...(2026-08-04)
• What Crushing Equipment Works Reliably at -40°C Without Brea...(2026-08-03)